Page 1 of 1
Messy arc sputter while welding aluminum
Posted: Thu Jul 30, 2026 8:54 pm
by 240sxbandit
Hello everyone, I have stumbled upon a problem when trying to weld any aluminum piece.
When I go to initiate the arc on my piece it can start ok but then one second after just starts to sputter on and off causing it to get a lot of contamination. Now I do clean and wipe down the piece with a brush and acetone , I have the the negative clamped onto my table and everything seems in order but for some reason it’s been doing this on some passes and I am deeply confused on why. I’ll post a link to show what I mean by the sputtering I am experiencing. Thank you for reading
https://youtube.com/shorts/s50p7Qh1LiQ? ... PEomtjAur_
Re: Messy arc sputter while welding aluminum
Posted: Fri Jul 31, 2026 1:05 am
by tweake
hi
can you post some pics of it?
what amps are you using? cup size? as many details as possible please.
from what i can see is your welding a thicker bit and its really really cold.
that could be from poor earthing. always best to earth directly to the work. tho i often use a third hand to bridge from work to table which i find helps a LOT.
Re: Messy arc sputter while welding aluminum
Posted: Fri Jul 31, 2026 6:57 am
by Jack Ryan
240sxbandit wrote: ↑Thu Jul 30, 2026 8:54 pm
I have the the negative clamped onto my table
Can you verify what you mean here please?
Jack
Re: Messy arc sputter while welding aluminum
Posted: Fri Jul 31, 2026 6:29 pm
by 240sxbandit
tweake wrote: ↑Fri Jul 31, 2026 1:05 am
hi
can you post some pics of it?
what amps are you using? cup size? as many details as possible please.
from what i can see is your welding a thicker bit and its really really cold.
that could be from poor earthing. always best to earth directly to the work. tho i often use a third hand to bridge from work to table which i find helps a LOT.
Hello and yes of course!
So machine is an everlast powertig 185dv
Using a #7 cup @12cfh
100 amps
3/32 ck green tungsten
Frequency @135
And balance @30
Yes I tried to pre heat but still had a bad ark. And I’ll try to earth straight to the work piece. As you mentioned the third arm idea is good cause it’s an oval shaped catch can so it’ll move around here and there . But thank you for the reply
Re: Messy arc sputter while welding aluminum
Posted: Fri Jul 31, 2026 6:32 pm
by 240sxbandit
tweake wrote: ↑Fri Jul 31, 2026 1:05 am
hi
can you post some pics of it?
what amps are you using? cup size? as many details as possible please.
from what i can see is your welding a thicker bit and its really really cold.
that could be from poor earthing. always best to earth directly to the work. tho i often use a third hand to bridge from work to table which i find helps a LOT.
Hello and yes of course!
So machine is an everlast powertig 185dv
Using a #7 cup @12cfh
100 amps
3/32 4043 filler rod
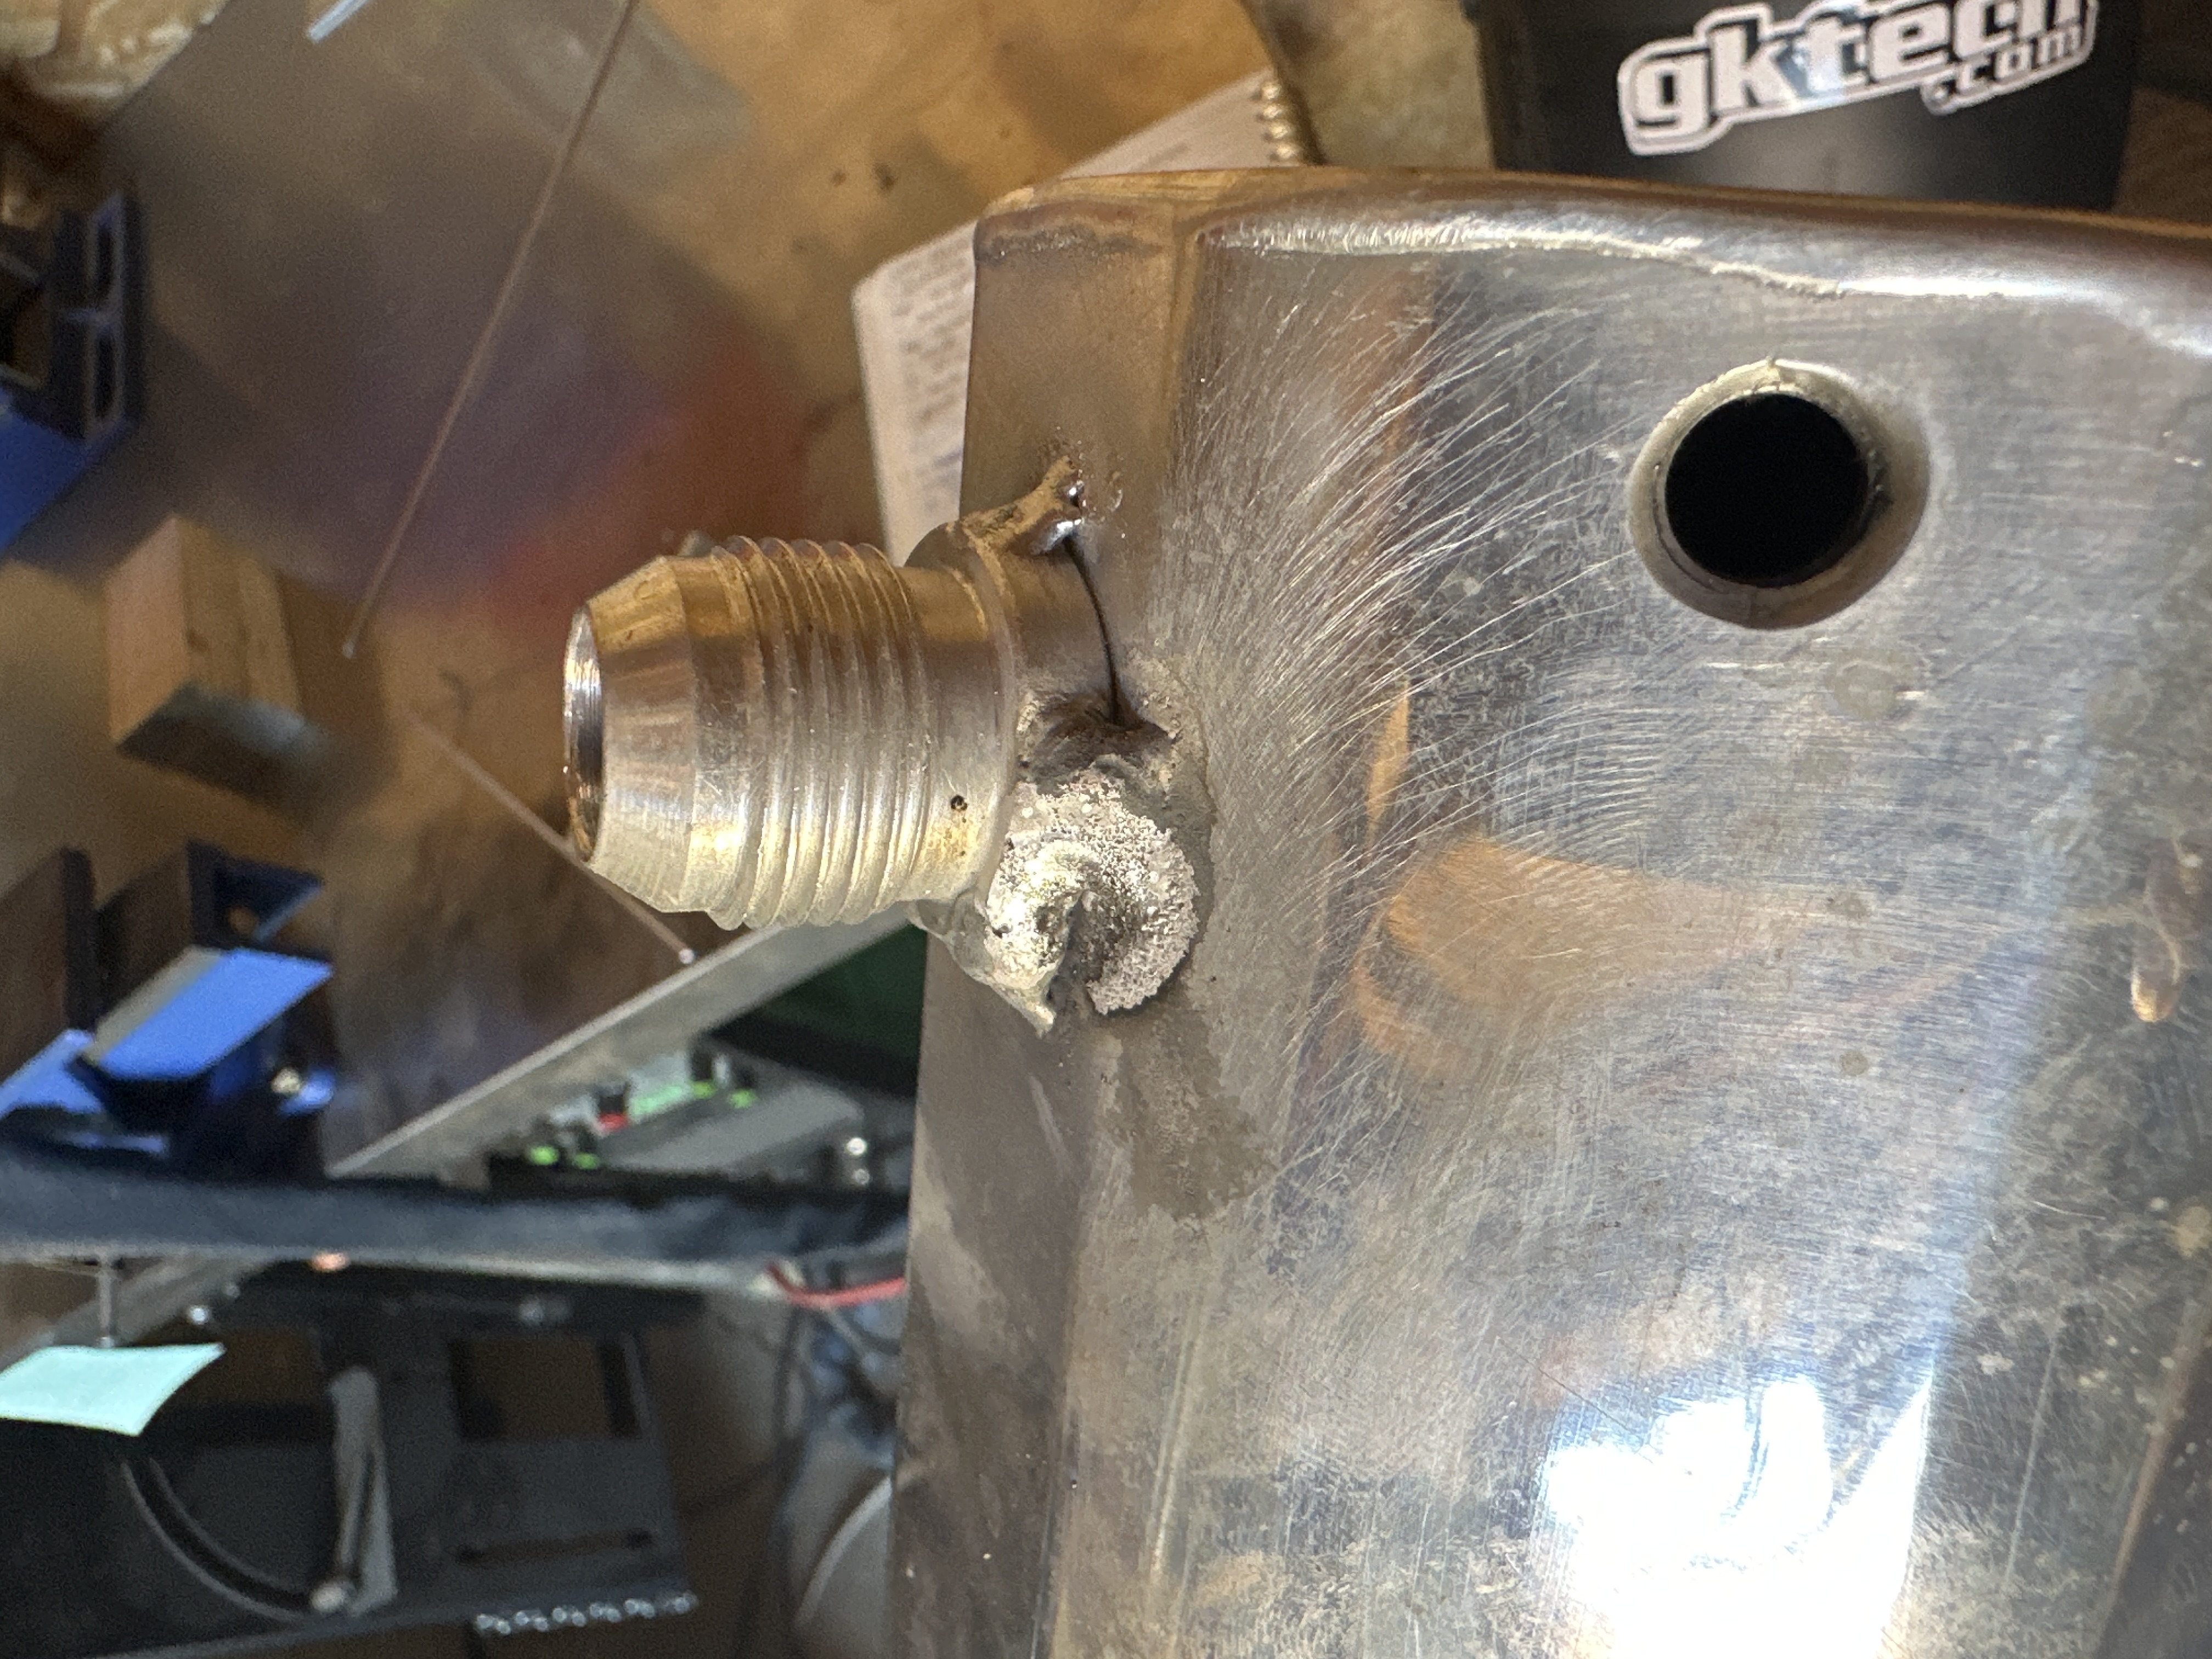
- image.jpg (2.72 MiB) Viewed 11339 times
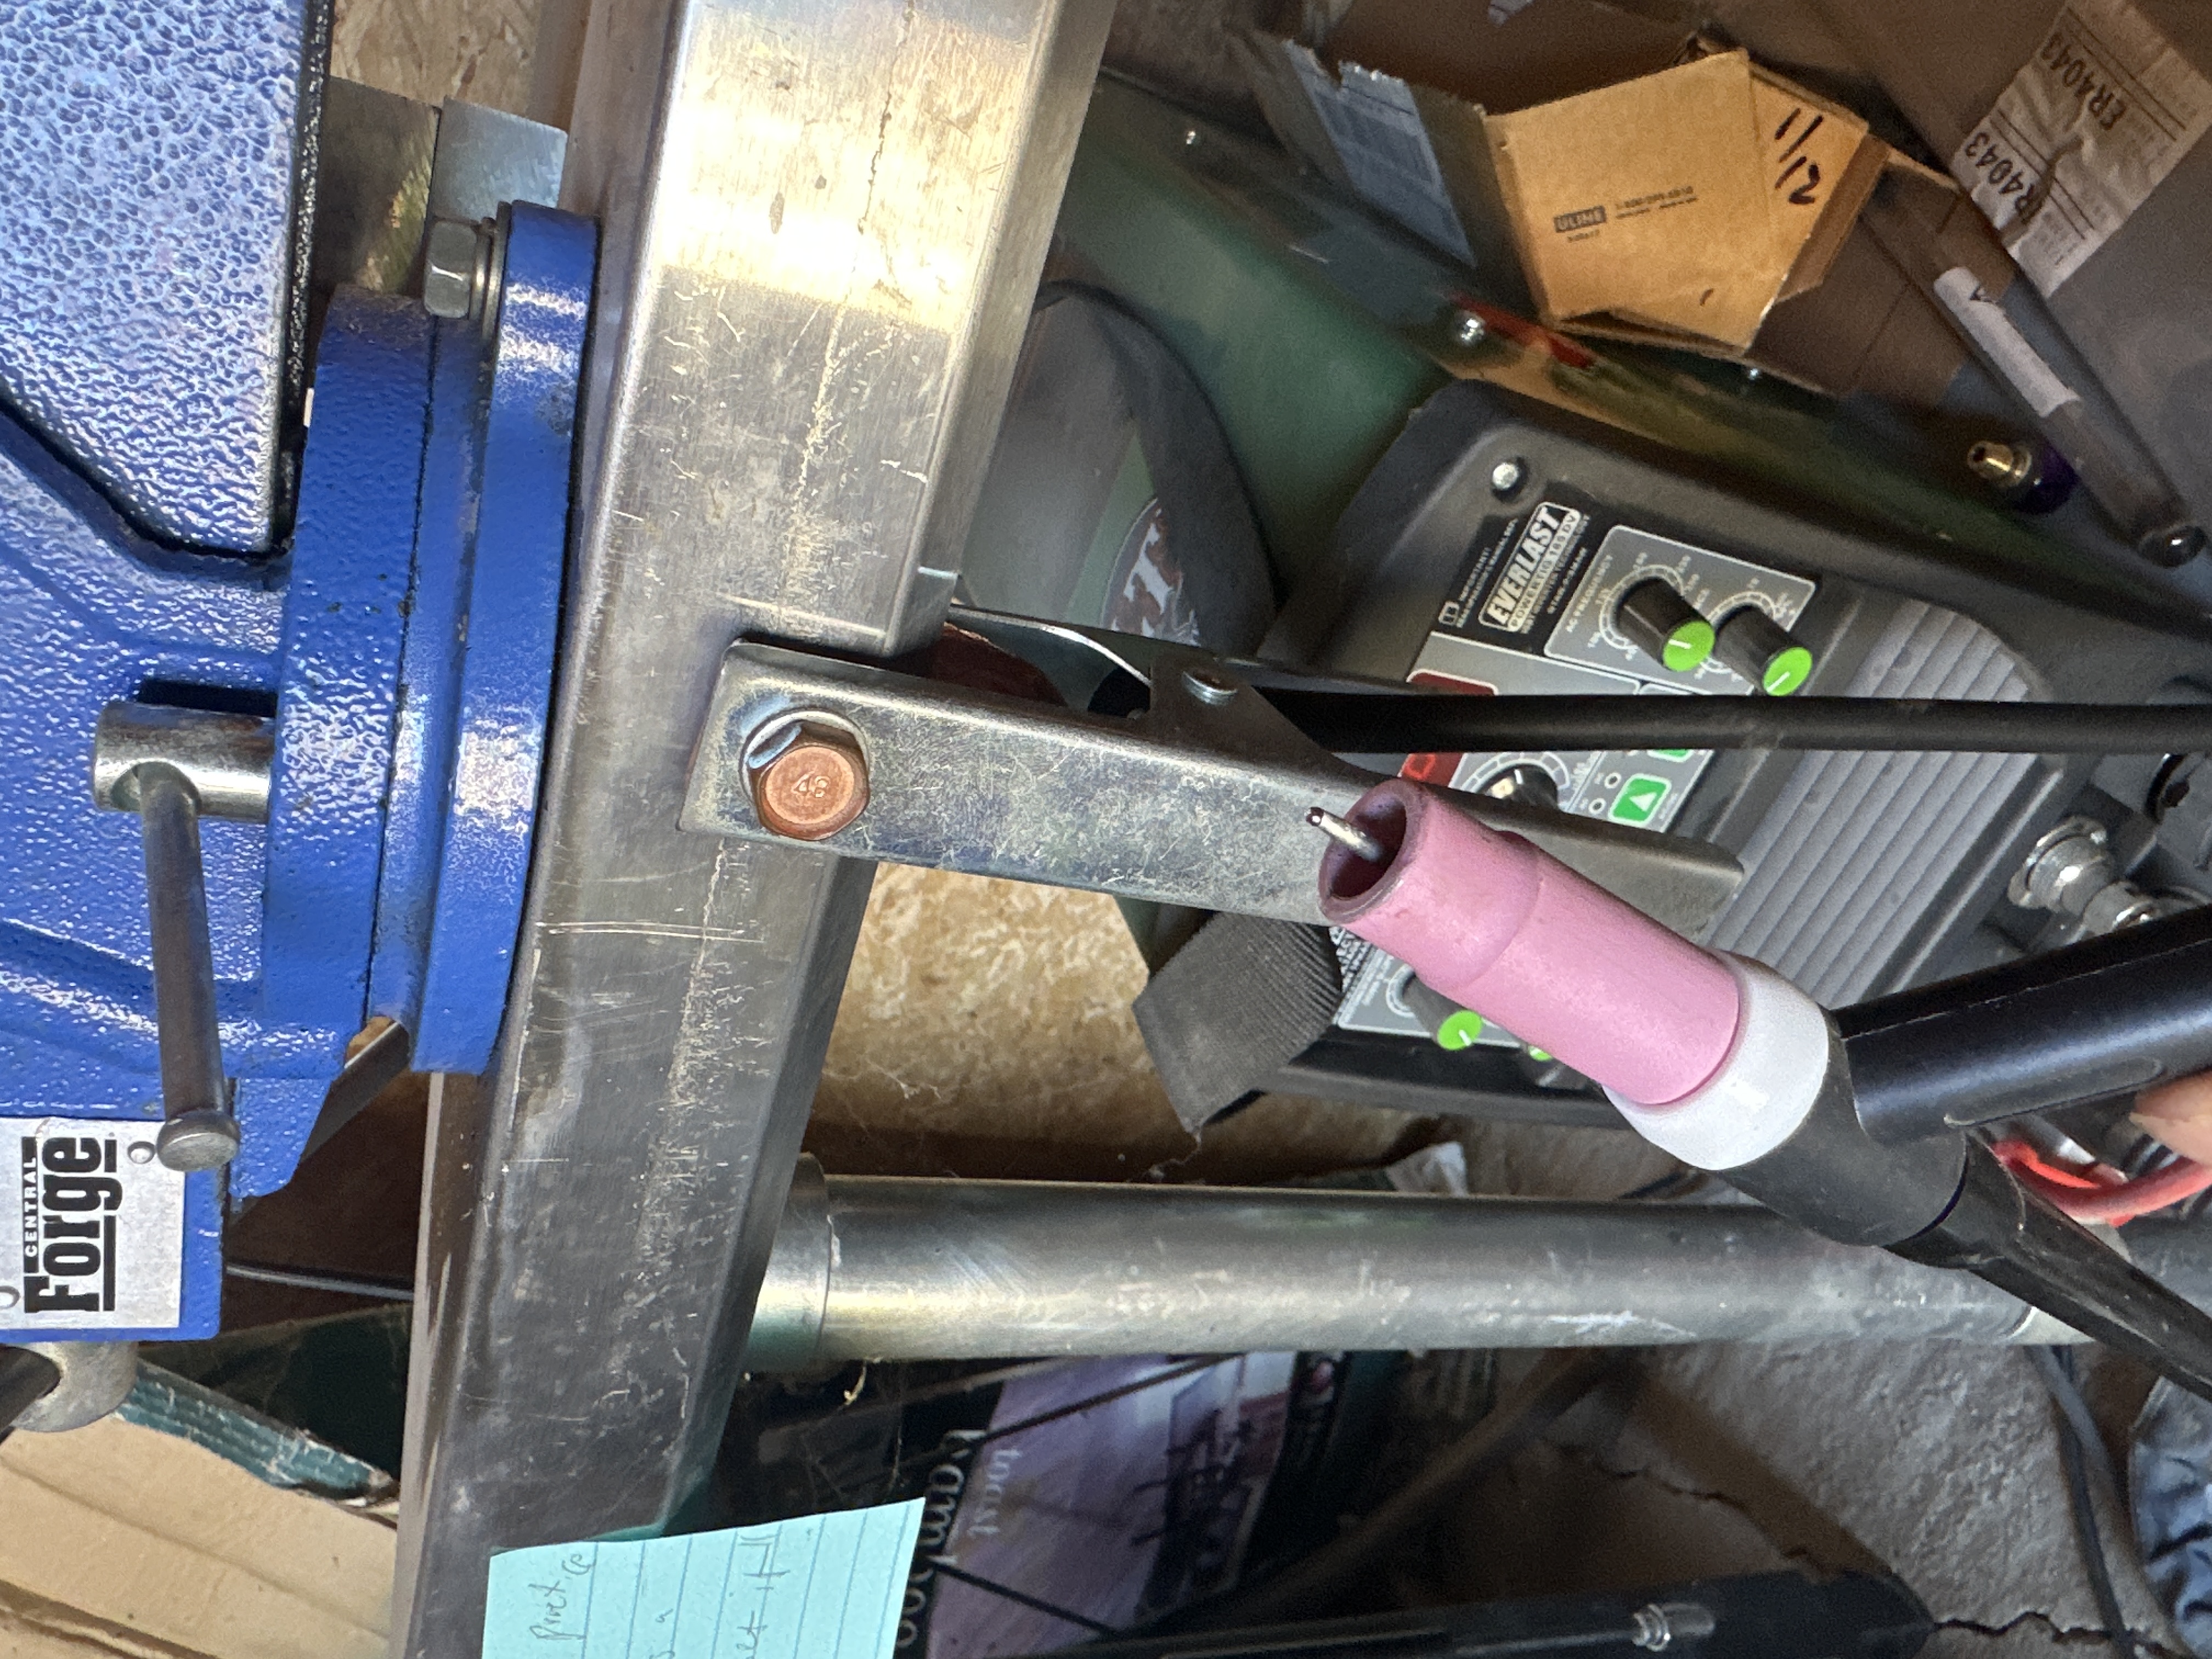
- image.jpg (2.99 MiB) Viewed 11339 times
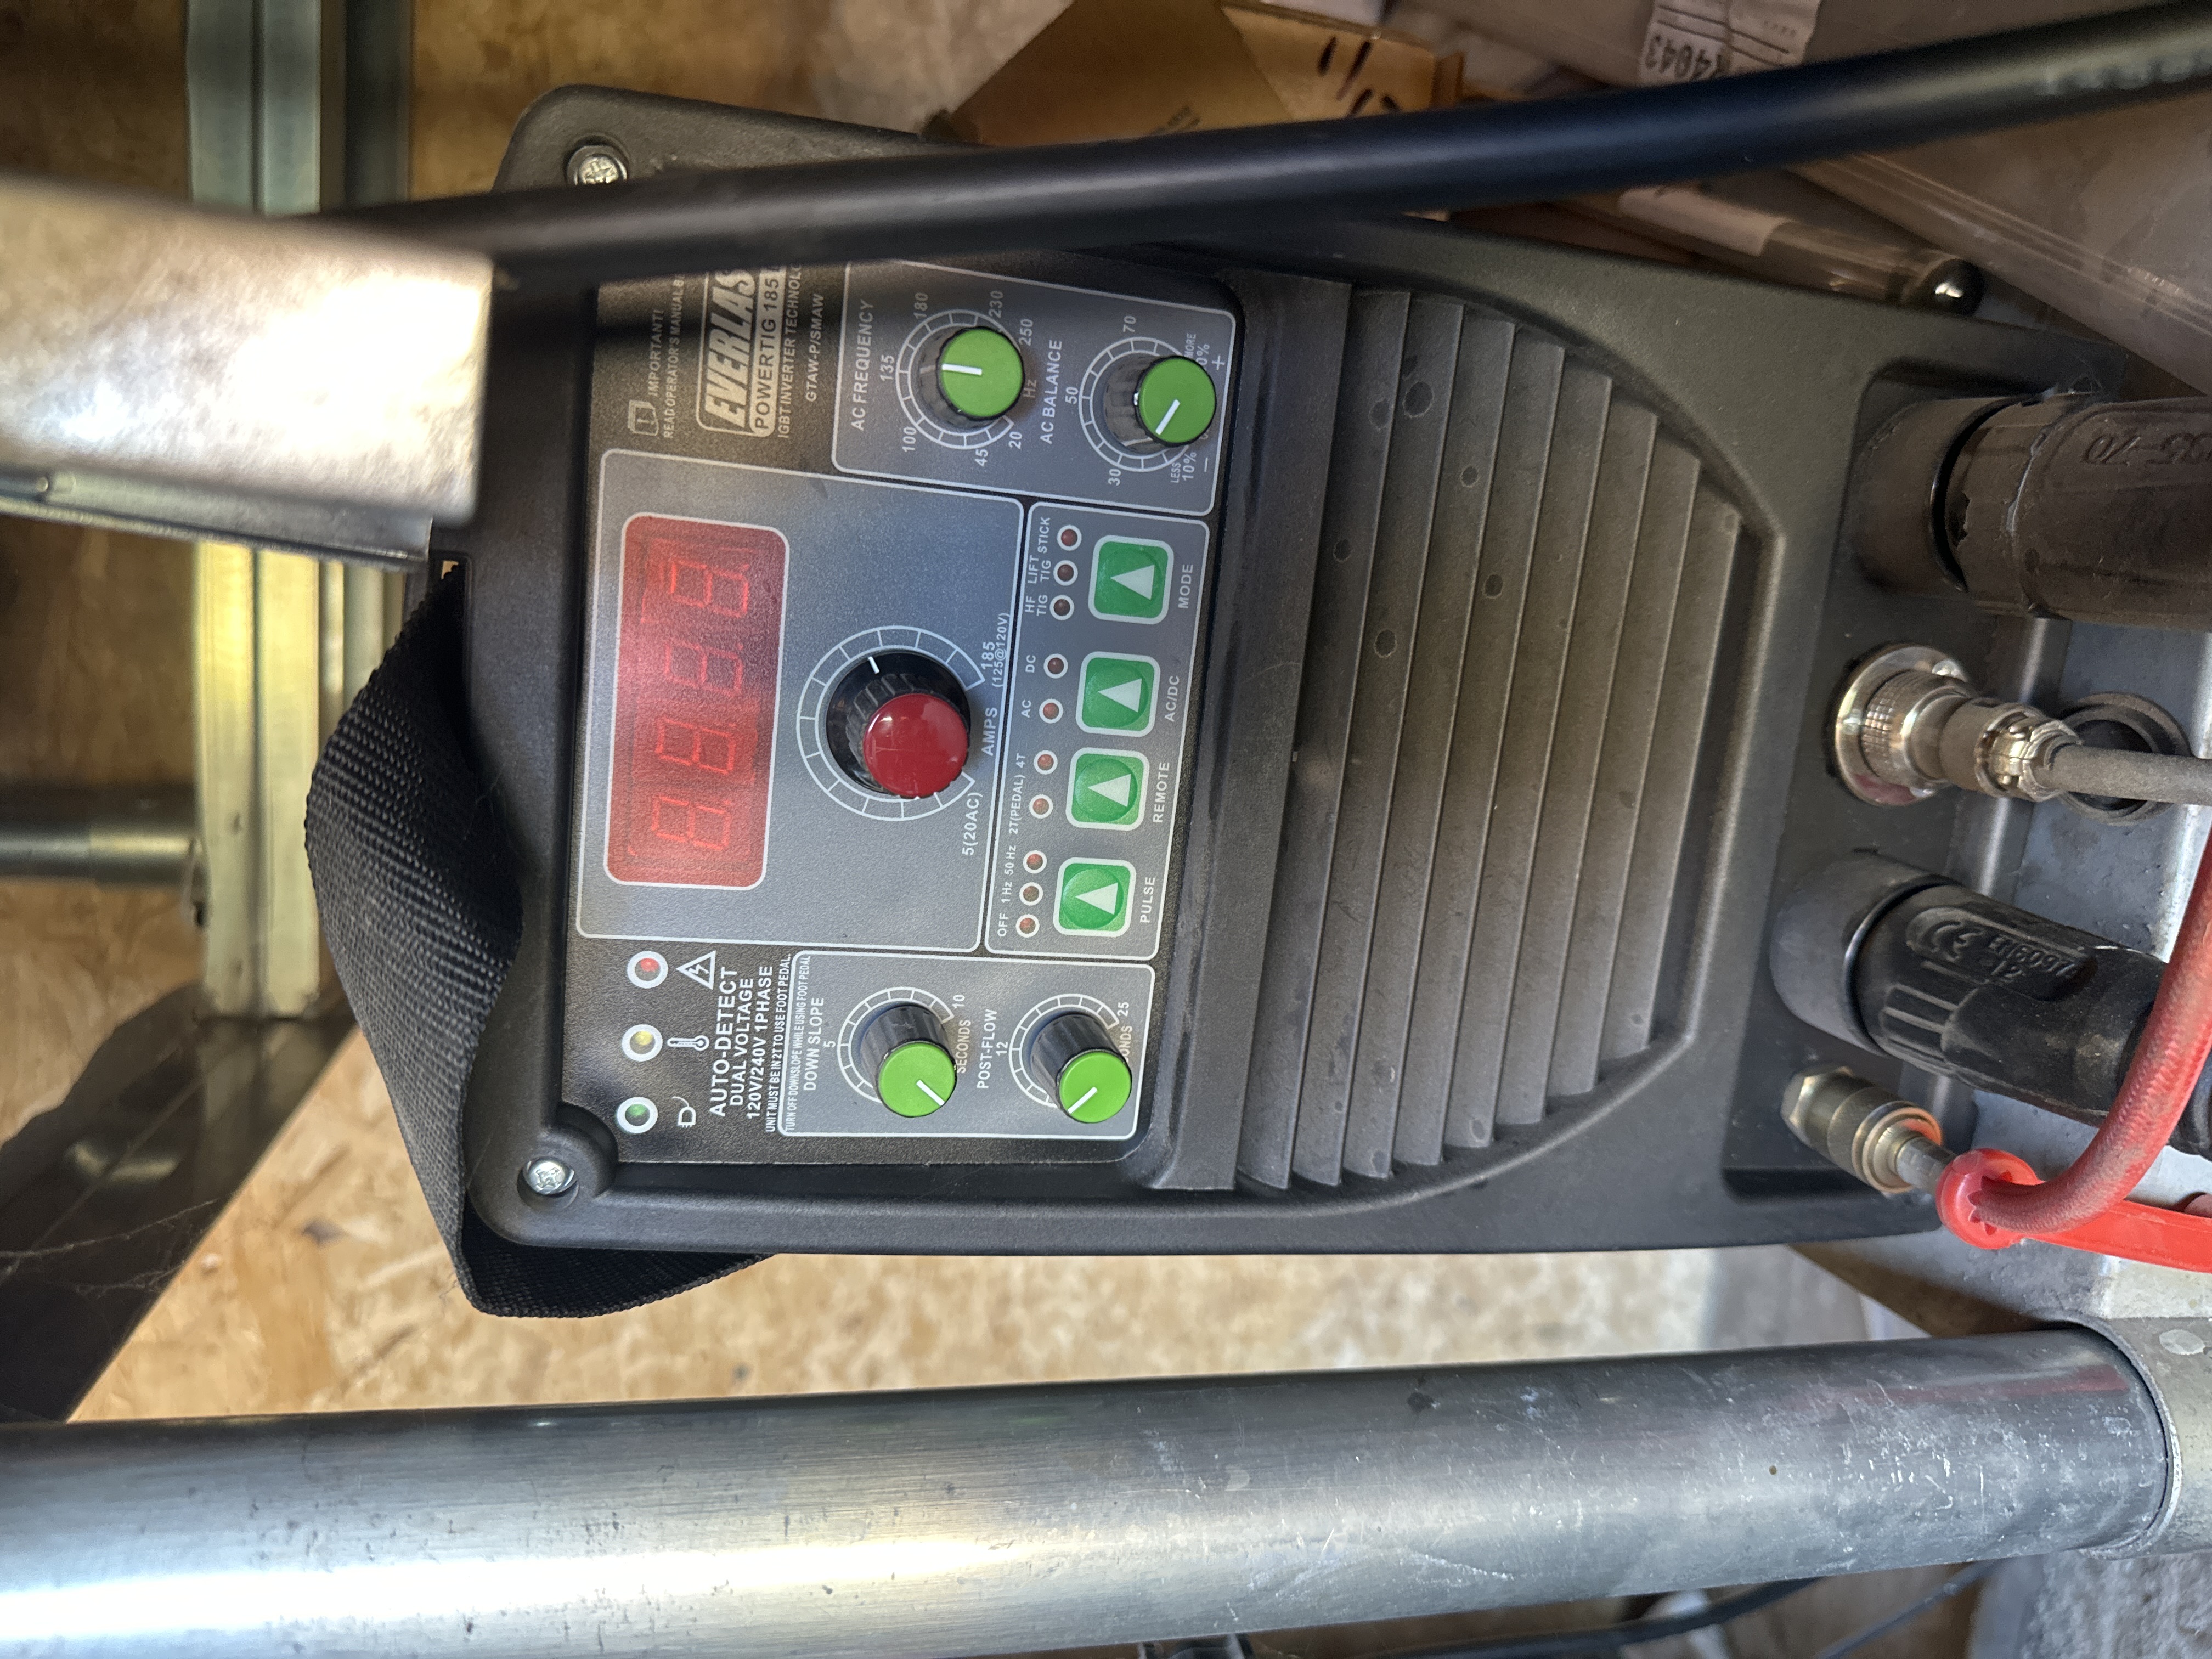
- image.jpg (2.81 MiB) Viewed 11339 times
3/32 ck green tungsten
Frequency @135
And balance @30
Yes I tried to pre heat but still had a bad ark. And I’ll try to earth straight to the work piece. As you mentioned the third arm idea is good cause it’s an oval shaped catch can so it’ll move around here and there . But thank you for the reply
Re: Messy arc sputter while welding aluminum
Posted: Fri Jul 31, 2026 9:49 pm
by Jack Ryan
240sxbandit wrote: ↑Thu Jul 30, 2026 8:54 pm
I have the the negative clamped onto my table
Can I say again, please clarify the polarity you are using.
If you are using electrode positive your balance will be inverted. So 30% cleaning will become 70% cleaning.
Jack
Re: Messy arc sputter while welding aluminum
Posted: Fri Jul 31, 2026 10:15 pm
by tweake
Jack Ryan wrote: ↑Fri Jul 31, 2026 6:57 am
240sxbandit wrote: ↑Thu Jul 30, 2026 8:54 pm
I have the the negative clamped onto my table
Can you verify what you mean here please?
Jack
good spotting
Re: Messy arc sputter while welding aluminum
Posted: Fri Jul 31, 2026 10:32 pm
by tweake
240sxbandit wrote: ↑Fri Jul 31, 2026 6:29 pm
tweake wrote: ↑Fri Jul 31, 2026 1:05 am
hi
can you post some pics of it?
what amps are you using? cup size? as many details as possible please.
from what i can see is your welding a thicker bit and its really really cold.
that could be from poor earthing. always best to earth directly to the work. tho i often use a third hand to bridge from work to table which i find helps a LOT.
Hello and yes of course!
So machine is an everlast powertig 185dv
Using a #7 cup @12cfh
100 amps
3/32 ck green tungsten
Frequency @135
And balance @30
Yes I tried to pre heat but still had a bad ark. And I’ll try to earth straight to the work piece. As you mentioned the third arm idea is good cause it’s an oval shaped catch can so it’ll move around here and there . But thank you for the reply
as Jack Ryan mentions, positive should be connected to the table. the tig torch is negative.
green tungsten is pure tungsten and is not recommended. however ck does use green packet for their layzr tungsten which is fine. taper make it fairly blunt. a fine taper will melt off and that could put tungsten in the weld and makes things a bit funky. you shouldn't be getting so much of a ball, but pure tungsten will do that, so will getting leads back to front. edit: light green is layzr, dark green is pure.
hard to tell what size that material is, but i would run at least 150 amps. or just set it to max and use the pedal to dial it down. you want a puddle to form in a few seconds.
funny enough if your to cold, you sit there to long and overheat the aluminium and 4043 goes to crap when overheated.
also i would drop cup size down to 5. have a bit more downslope and have a lot more post flow. you need the gas flow to keep the tungsten clean as it cools down.
hopefully that helps at least get the basics reasonable and then see if the problem is still happening.
Re: Messy arc sputter while welding aluminum
Posted: Fri Jul 31, 2026 10:41 pm
by 240sxbandit
Jack Ryan wrote: ↑Fri Jul 31, 2026 9:49 pm
240sxbandit wrote: ↑Thu Jul 30, 2026 8:54 pm
I have the the negative clamped onto my table
Can I say again, please clarify the polarity you are using.
If you are using electrode positive your balance will be inverted. So 30% cleaning will become 70% cleaning.
Jack
Yeah I apologize totally missed that. Just checked have earth on positive and negative on my electrode.
Re: Messy arc sputter while welding aluminum
Posted: Sat Aug 01, 2026 1:45 pm
by BillE.Dee
Torch negative. I'm thinkin you got the wrong polarity goin on.
Re: Messy arc sputter while welding aluminum
Posted: Sun Aug 02, 2026 7:33 am
by cj737
BillE.Dee wrote: ↑Sat Aug 01, 2026 1:45 pm
Torch negative. I'm thinkin you got the wrong polarity goin on.
He already confirmed DCEN. The problem is simply too little amps and in my experience too low of CFM. Tweake encouraged cup size #5, I’d go that route too since your #7 is a collet body style and not a gas lens.
With a #7 crank the gas up to 15-18 CFM, 150 amps. Arc pointed at base until it starts to wet, then up onto bung, then right at the gap before you add filler.
Another issue is the edge of the tube. It creates a split in gas coverage so you get interrupted shielding. Keep the arc really pointed directly at the gap. Too much “vertical” angle and you’ll have no shielding as you come around the side of the bung where the tube overlap is the most narrow.
Bump up to 75%-78% for better results on your penetration.
Re: Messy arc sputter while welding aluminum
Posted: Thu Aug 13, 2026 2:41 pm
by pavetim
Green tungsten is not made for inverter machines. Get some layzr, E3 or throated, or even 2% lanthanated.
Re: Messy arc sputter while welding aluminum
Posted: Tue Aug 18, 2026 3:25 pm
by BillE.Dee
I have the the negative clamped onto my table. ( by OP).
cj, shouldn't the torch be in the negative connector? And my green machines are oppossite of miller for balance.
Re: Messy arc sputter while welding aluminum
Posted: Tue Aug 18, 2026 3:26 pm
by BillE.Dee
On my green machine when welding ally, my torch is in negative and my balance is about 9 o'clock. Opposite of miller
Re: Messy arc sputter while welding aluminum
Posted: Wed Aug 19, 2026 4:50 pm
by cj737
BillE.Dee wrote: ↑Tue Aug 18, 2026 3:25 pm
I have the the negative clamped onto my table. ( by OP).
cj, shouldn't the torch be in the negative connector? And my green machines are oppossite of miller for balance.
I don’t know “green machines” but I do know polarity. Yes, for steel, torch needs to be in a “NEG” plug so that you run DCEN. But he’s welding ally, so that’s AC, switching between polarities. On my Miller Dynasty, it’s one plug, a button to swap polarity.
Re: Messy arc sputter while welding aluminum
Posted: Thu Aug 20, 2026 4:54 am
by tweake
cj737 wrote: ↑Wed Aug 19, 2026 4:50 pm
I don’t know “green machines” but I do know polarity. Yes, for steel, torch needs to be in a “NEG” plug so that you run DCEN. But he’s welding ally, so that’s AC, switching between polarities. On my Miller Dynasty, it’s one plug, a button to swap polarity.
even on AC its needs to be correctly connected as each side of the waveform is not equal in a lot of inverters. thats adjustable in the really fancy machines.
Re: Messy arc sputter while welding aluminum
Posted: Thu Aug 20, 2026 6:43 am
by Jack Ryan
tweake wrote: ↑Thu Aug 20, 2026 4:54 am
cj737 wrote: ↑Wed Aug 19, 2026 4:50 pm
I don’t know “green machines” but I do know polarity. Yes, for steel, torch needs to be in a “NEG” plug so that you run DCEN. But he’s welding ally, so that’s AC, switching between polarities. On my Miller Dynasty, it’s one plug, a button to swap polarity.
even on AC its needs to be correctly connected as each side of the waveform is not equal in a lot of inverters. thats adjustable in the really fancy machines.
If the "polarity" is wrong, the AC balance gets inverted. The torch plugs into the negative terminal - even for AC.
Jack