Boyracer wrote:I mis-spoke on the tungsten size. I'm using 1/16" and a 17 torch. The welder is a Lincoln Square Wave 175.
It seems like I'm putting a lot of heat into the joint. Am I not moving fast enough?
Yup exactly that. I started out on tubing and should have practiced a bit more. It's never too late, since I'm doing a lot of practice followed by then cutting out the welded section and butt'ing them up again to go at it.
A 1/16" tungsten is perfect. Grind the tip around 3/16" long (3x the diameter) and just barely knock-off the needle-tip if you're left with one. Order a #8 stubby gas lens from HTP, they have it for about $20. You can extend the tungsten a little bit further and you need all the coverage you can get with tubing with such a small curvature----argon dissipates MUCH quicker on small tubing than any other surface besides an outside corner joint.
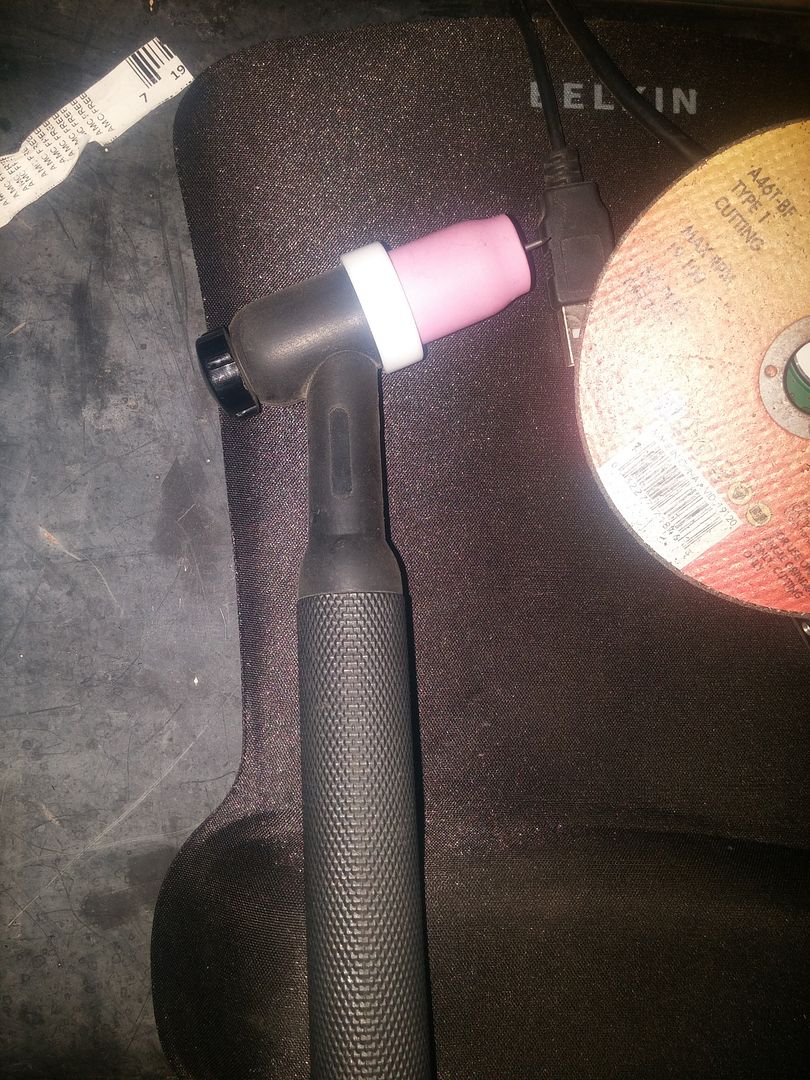
This is a WP17 with a stubby gas lens, #8 cup, and short back cap
One thing that plagued me, is arc length consistency. You need to hold a tight arc (< 1/16") and you need to
maintain it the whole way throughout. Otherwise, all the tiny up-down variations in your hand are directly translated into the arc length, and an increasing arc length = excess voltage = more heat dumped into the part. Also, you need to be using 0.045" diameter filler or even 0.035". Lose the 1/16" filler rod if that's what you're using. You need more amperage to melt the filler than the base metal using 1/16" filler rod, which in turn will cause even more overheating.
Moving fast will only help you if you can nail down the correct torch angle. Try a dry "fast run", but stop yourself right in the middle of it, and freeze your torch hand. Take a "step back" and look at the angle, honestly. Is it where it needs to be? Hopefully so, but if not, you need to go back to square-1 and really dial in your concentration.